In the modern landscape of metal container manufacturing, the efficiency of production lines is dictated by the precision of the equipment used. For enterprises specializing in the fabrication of chemical drums, paint buckets, and stainless steel containers, the integration of high-performance welding and shaping technology is paramount. Understanding the optimal bending machine use and its synergy with advanced laser seam welding allows manufacturers to scale their operations while maintaining rigorous quality standards.
Global demand for durable metal packaging continues to rise, driven by the chemical and industrial oil sectors. To meet this demand, the transition from traditional resistance welding to laser-based butt welding represents a significant technological leap. This shift eliminates many of the material restrictions and surface preparation requirements that previously slowed down production cycles, providing a more versatile approach to barrel construction.
For barrel-making enterprises with a wide variety of product lines, the ability to handle different diameters, thicknesses, and materials without constant re-tooling is the ultimate competitive advantage. By optimizing bending machine use and laser welding integration, factories can now produce everything from small vacuum cleaner casings to large industrial oil drums with unprecedented stability and reliability.
The Role of Laser Seam Welding in Metal Barrel Production
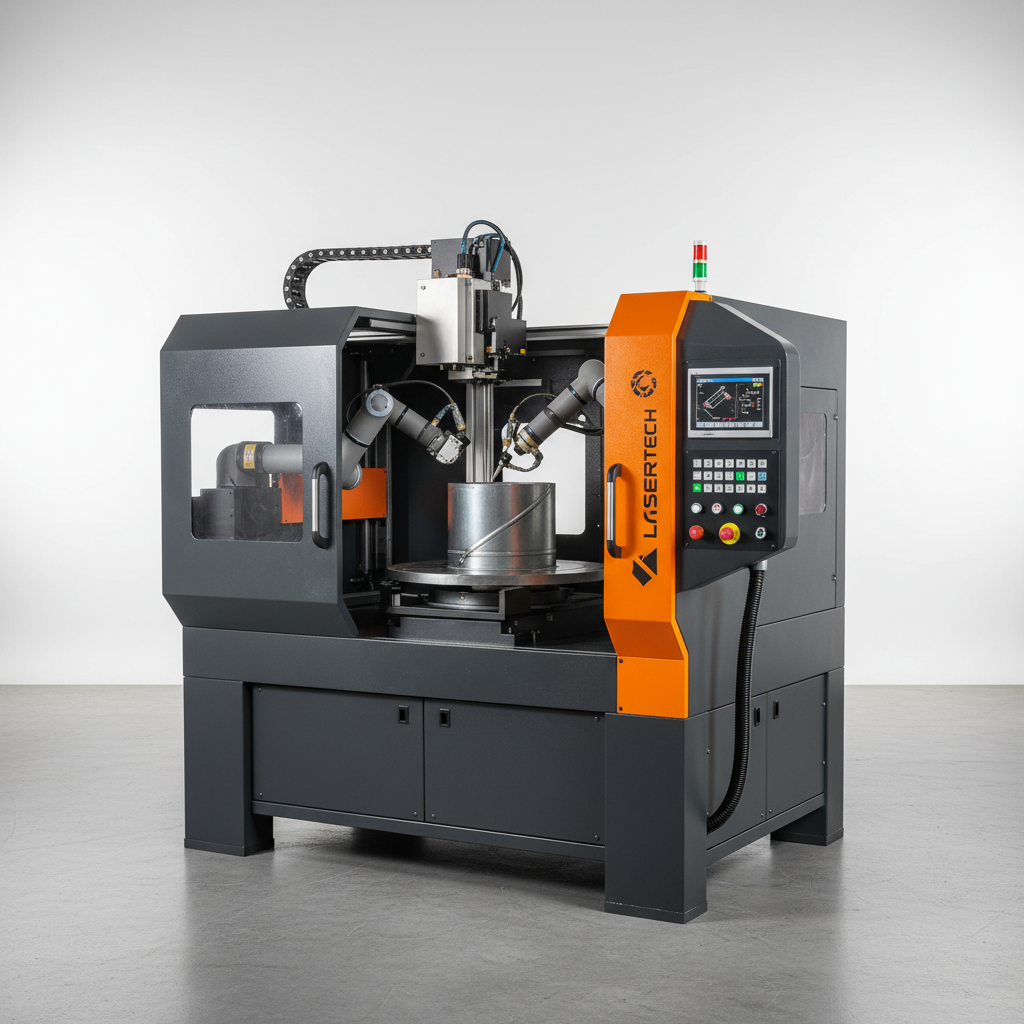
The laser fully automatic seam welding machine is specifically engineered for the metal barrel industry, providing a seamless solution for welding various container types. Unlike traditional methods, this technology focuses on butt welding, which allows for the production of high-quality chemical barrels, paint drums, and stainless steel soup barrels without the rigid restrictions typically associated with industrial metal joining.
By integrating this technology, manufacturers can enhance their bending machine use workflows, ensuring that once the metal is shaped, the final seam is perfectly airtight and aesthetically pleasing. The process is supported by nitrogen protection, which prevents oxidation and ensures a clean, professional finish on every single unit produced.
Overcoming Material and Surface Constraints
One of the most significant challenges in metal container fabrication is the surface condition of the raw materials. Traditional resistance welding requires pristine surfaces to ensure electrical conductivity and weld integrity, which often necessitates costly and time-consuming cleaning processes.
In contrast, laser welding is not dependent on resistance heat but relies on concentrated laser energy. This means that surface contaminants such as rust, oil stains, dust, and impurities do not affect the quality of the butt weld. Whether the steel plates are galvanized, coated, printed, or stainless steel with protective films, the laser penetrates and joins the material effectively.
This capability is a major breakthrough for enterprises that handle a wide variety of steel barrel products. It reduces the need for pre-treatment and minimizes the risk of weld failure due to surface impurities, thereby streamlining the overall production cycle and reducing waste.
Flexibility in Diameter and Thickness Handling
The versatility of laser welding machines allows them to handle steel drums of virtually any diameter. This is achieved because the system utilizes a positioning robot to hold the welding edge and bring the two sides together, rather than relying on the restrictive waist drum wheel positioning technology used in older equipment. This means that even if there are slight errors in the cutting size, the bending machine use remains efficient and the weld remains precise.
Thickness adaptability is another core advantage. While the standard thickness for steel drums typically ranges between 0.6mm and 1.5mm (with 0.9mm to 1.2mm being most common), laser welding machines are not sensitive to these variations. As long as the adjustable laser power is sufficient, the machine can weld significantly thicker steel drums without a loss in quality.
This adaptability simplifies the production floor, as a single machine can be adjusted via simple speed and power regulations to accommodate different product specifications. For companies offering a diverse catalog of containers, this flexibility reduces the need for multiple specialized machines, optimizing the total bending machine use within the factory layout.
Operational Efficiency and Automation Benefits
Modern laser welding systems are designed to be user-friendly and highly efficient, removing the reliance on intensive manual labor. The entire operation is governed by a microcomputer and servo speed regulation, ensuring that the welding process is stable, reliable, and repeatable across thousands of cycles.
The integration of automation not only speeds up the production of industrial buckets and oil drums but also ensures a level of precision that manual welding cannot match. The synergy between the positioning robot and the laser head minimizes human error, resulting in higher yields and lower scrap rates.
Comparison of Laser Welding Performance Metrics
Broad Material Compatibility and Hybrid Welding
Unlike resistance welding, which is limited by the electrical resistivity of the material, laser welding is independent of such properties. This allows it to weld not only various grades of steel but also low-resistance materials like copper and aluminum, which are traditionally difficult to join using resistance-based methods.
Furthermore, the laser system enables the welding of different metal materials together, opening up new possibilities for hybrid container designs. This capability ensures that regardless of the material choice for the barrel, the bending machine use and subsequent welding phase remain seamless and effective.
Industrial Application Scenarios and Use Cases
The versatility of the laser fully automatic seam welding machine makes it ideal for a wide range of industrial products. From the production of chemical buckets and industrial oil drums to the fabrication of specialized vacuum cleaner casings, the technology adapts to the specific needs of each container type.
In the paint industry, where barrels must be perfectly sealed to prevent solvent leakage, the laser's precision ensures a leak-proof joint. Similarly, in the food industry, stainless steel soup barrels benefit from the clean, nitrogen-protected weld, which prevents contamination and ensures hygiene standards are met.
Whether it is a small-scale boutique manufacturer or a large-scale industrial plant, the ability to switch between different barrel sizes and materials without extensive downtime makes this equipment an essential asset for any modern metal container production line.
Comparative Analysis of Laser vs Resistance Welding
Comparing laser welding to resistance welding reveals a fundamental difference in how energy is applied. Resistance welding relies on the material's own electrical resistance to generate heat, which makes it hypersensitive to surface cleanliness, material thickness, and the resistivity of the metal.
Laser welding, by contrast, uses an external heat source that is precisely focused. This removes the need for diameter-based positioning wheels and allows for a much wider range of materials, including aluminum and copper. The resulting joint is often stronger and visually superior.
For the modern manufacturer, the choice is clear: laser technology provides the scalability and reliability needed to compete in a global market. By optimizing the bending machine use and integrating laser seam welding, factories can achieve higher throughput with lower operational risks.
Key Technical Differences: Laser Welding vs. Resistance Welding
| Feature |
Laser Welding |
Resistance Welding |
Production Impact |
| Surface Requirement |
Tolerates oil, rust, and coatings |
Requires clean, conductive surface |
Lower pre-treatment cost |
| Material Range |
Steel, Aluminum, Copper, Alloys |
Primarily conductive steels |
Higher product diversity |
| Positioning Method |
Robot-edge holding |
Waist drum wheel positioning |
Faster changeovers |
| Thickness Sensitivity |
Low (Adjustable power) |
High (Strict limits) |
Flexible SKU management |
| Weld Aesthetics |
Clean, nitrogen-protected |
Variable, often requires grinding |
Reduced finishing time |
| Control System |
Microcomputer & Servo |
Manual or Basic Timer |
Consistent quality control |
FAQS
Yes, unlike resistance welding, laser welding does not rely on the electrical conductivity of the surface. It can weld galvanized, coated, and printed plates, as well as stainless steel with protective films, without these factors affecting the joint quality.
Because the laser welding machine uses a positioning robot to hold the edges rather than diameter-based waist drum wheels, it is not limited by diameter positioning. Slight cutting errors will not affect the welding process, ensuring a stable joint.
Absolutely. Since laser welding is not dependent on the material's resistivity, it can easily weld low-resistance materials like copper and aluminum, and it can even join two different types of metal together.
The machine is highly adaptable to thickness changes. While most drums are between 0.9mm and 1.2mm, the laser power is adjustable, allowing it to weld thicknesses from 0.6mm up to significantly thicker steel plates without losing precision.
Nitrogen protection prevents the weld seam from oxidizing during the high-heat process. This results in a more aesthetically pleasing, clean, and corrosion-resistant joint, which is critical for chemical and food-grade containers.
No, the system is designed for full automation. It is controlled by a microcomputer with servo speed regulation, making the operation user-friendly and removing the need for constant manual intervention.
Conclusion
The evolution of metal container manufacturing is defined by the transition toward automation and the removal of material constraints. By integrating laser fully automatic seam welding, manufacturers can overcome the limitations of surface contamination, material resistivity, and rigid diameter positioning. This technological leap, combined with a strategic approach to bending machine use, enables the production of high-quality industrial buckets, oil drums, and specialized casings with unmatched efficiency and aesthetic precision.
Looking forward, the adoption of laser-based systems will be the primary differentiator for enterprises seeking to scale their production while diversifying their product offerings. We recommend that barrel-making companies invest in servo-controlled, microcomputer-managed equipment to ensure long-term reliability and competitiveness in the global market. To explore these high-performance solutions further, visit our website: www.xdrmachine.com.
 8613931787312
 Botou Industrial Zone on the east side of National Highway 104, Botou City, Hebei Province